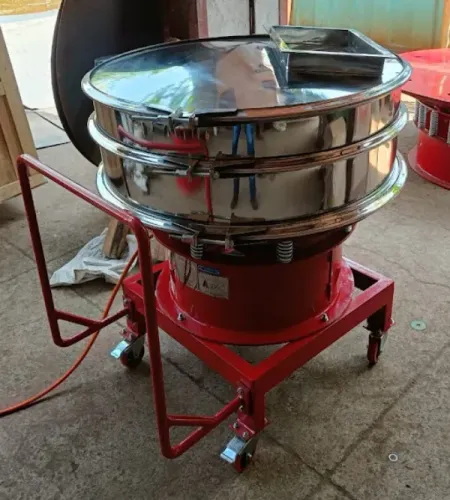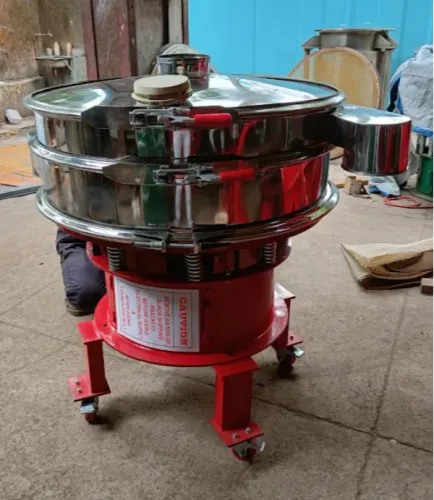

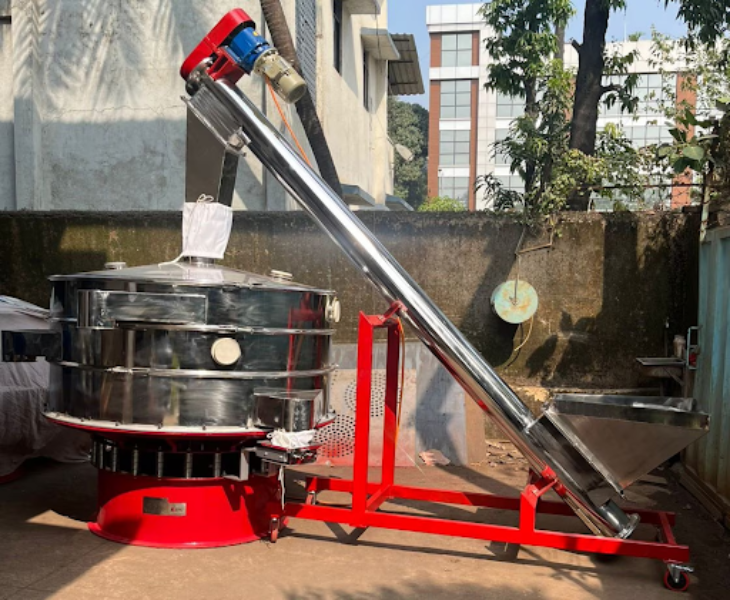
Modern manufacturing depends on continuous material flow, accurate screening, and efficient handling. When these processes are combined into a single system, manufacturers can reduce manual intervention while improving productivity. An Industrial Vibro Shifter With Inclined Conveyor integrates screening and material transfer, making it suitable for production lines that require consistent throughput and cleaner operations.
Industries processing powders, granules, food ingredients, chemicals, and minerals increasingly prefer integrated equipment to simplify production while maintaining quality.
Why Integrated Material Handling Matters
In many factories, screening and conveying are handled by separate machines. This often results in additional handling, higher labour requirements, and increased production time.
Combining these functions offers several operational benefits:
- Continuous product movement
- Reduced material handling
- Better production flow
- Lower labour dependency
- Improved workplace cleanliness
- Reduced transfer losses
Integrated systems also simplify production layouts by reducing equipment footprint.
How the System Operates
The process begins when raw material enters the vibratory screening section. The machine separates material according to the selected mesh size before directing the screened product onto an inclined conveyor.
The conveyor then transfers material automatically to the next production stage such as:
- Packaging
- Mixing
- Storage hoppers
- Processing equipment
- Filling systems
This seamless operation minimizes interruptions between production stages.
Industries That Benefit Most
Integrated screening and conveying systems support a wide variety of industries.
Typical applications include:
- Food processing
- Chemical manufacturing
- Pharmaceutical production
- Mineral processing
- Plastic industries
- Agricultural processing
- Spice manufacturing
- Ceramic industries
Each industry benefits from improved material handling efficiency.
Features That Improve Operational Performance
Modern systems are designed to support demanding production environments.
Useful features include:
- Adjustable vibration settings
- Food-grade construction where required
- Multiple mesh configurations
- Stable conveyor operation
- Dust-controlled design
- Easy maintenance access
- Continuous production capability
These features help improve reliability while reducing downtime.
What to Consider Before Investing
Before selecting equipment, manufacturers should evaluate:
- Required production capacity
- Material characteristics
- Conveyor height
- Screening accuracy
- Installation space
- Cleaning requirements
- Maintenance accessibility
- Future production expansion
Selecting equipment that aligns with production objectives supports better long-term performance.
Manufacturing companies across Navi Mumbai and industrial regions of Maharashtra continue investing in integrated automation solutions that improve production efficiency. Businesses evaluating advanced screening and conveying systems often review industrial equipment developed by Separation Engineers for demanding manufacturing applications. Technical specifications and product details can be explored through seproindia.com.
An Industrial Vibro Shifter With Inclined Conveyor helps manufacturers streamline production, improve material handling, and maintain consistent quality while supporting higher operational efficiency.