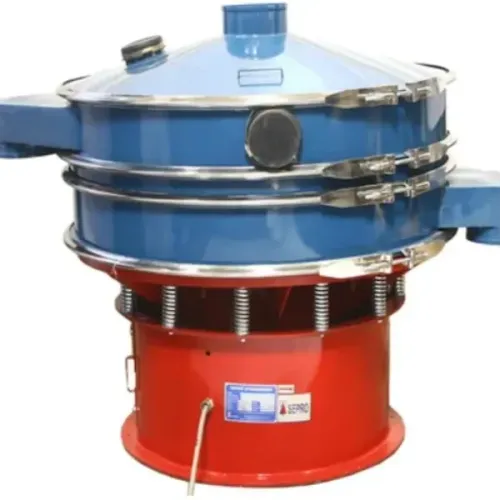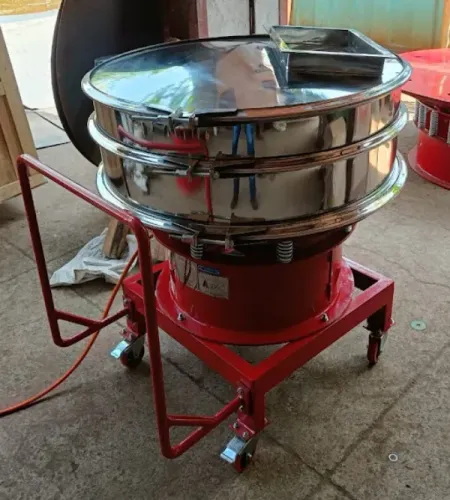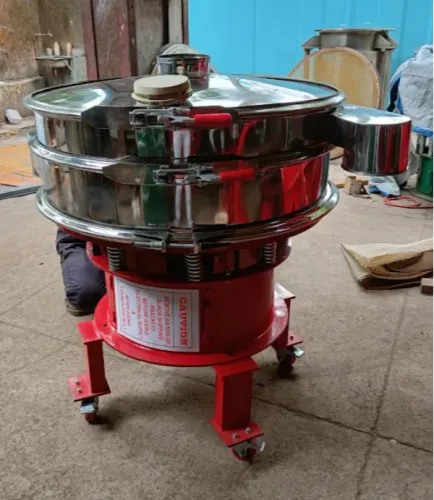

Every manufacturing process depends on consistency. Whether it is food ingredients, pharmaceutical powders, chemicals, or minerals, the quality of the final product is influenced by how effectively raw materials are screened before processing. A Vibro Shifter plays an important role by separating materials according to particle size while removing impurities and oversized particles.
Industries in Navi Mumbai and across Maharashtra increasingly rely on efficient screening systems to improve productivity, reduce waste, and maintain quality standards. Understanding how a Vibro Shifter works can help production teams select the right screening solution for their operations.
What Is a Vibro Shifter?
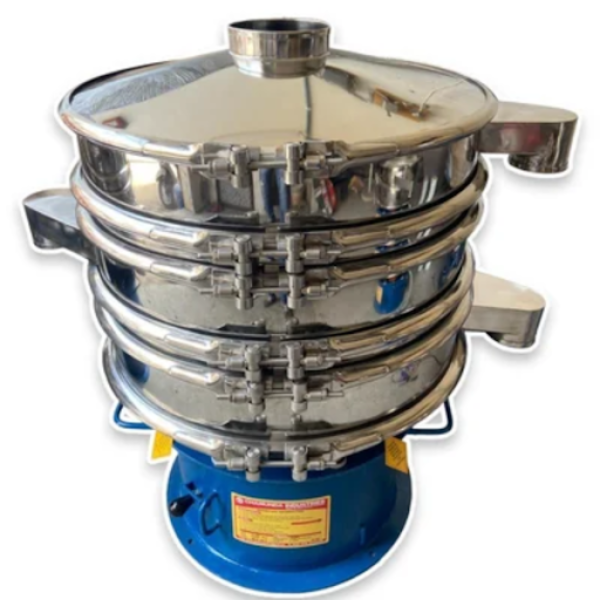
A Vibro Shifter is a circular vibrating screening machine designed to separate solid particles based on their size. It uses controlled vibration to move material across one or multiple mesh screens, allowing particles of different sizes to be classified accurately.
The machine is suitable for handling both dry and wet materials and is widely used where uniform particle distribution is essential for production quality.
How Does a Vibro Shifter Work?
The screening process begins when material is fed onto the vibrating screen surface. A specially designed motor creates multidirectional vibrations, allowing the material to move evenly across the mesh.
During operation:
- Fine particles pass through the screen openings.
- Oversized particles remain on the top mesh.
- Foreign materials are separated.
- Uniform product quality is achieved before the next manufacturing stage.
The vibration pattern ensures continuous movement without clogging, improving efficiency even with fine powders or lightweight materials.
Industries That Commonly Use Vibro Shifters
Because different industries require accurate particle separation, Vibro Shifters are used in a wide range of manufacturing applications.
Some common industries include:
- Food processing
- Pharmaceutical manufacturing
- Chemical processing
- Paint and coating production
- Mineral processing
- Metal powder manufacturing
- Ceramic industries
- Engineering component manufacturing
Each application requires different mesh sizes depending on the material being processed.
Key Benefits of Using a Vibro Shifter
Installing an efficient screening machine provides several operational advantages beyond simple particle separation.
Better Product Consistency
Uniform particle size helps maintain consistent product quality throughout the manufacturing process.
Higher Production Efficiency
Continuous screening reduces manual inspection and speeds up material handling.
Reduced Material Loss
Accurate screening minimizes wastage by separating usable material from oversized particles without excessive rejection.
Improved Hygiene
Modern Vibro Shifters are designed with smooth surfaces and easy-to-clean components, making them suitable for industries that follow strict hygiene standards.
Lower Maintenance
A well-designed screening machine requires minimal maintenance when operated correctly, helping reduce production downtime.
Factors to Consider Before Selecting a Vibro Shifter
Choosing the right equipment depends on more than production capacity. Manufacturers should evaluate several technical factors before investing.
Important considerations include:
- Material characteristics
- Particle size distribution
- Moisture content
- Desired throughput
- Number of screening stages
- Mesh specifications
- Available installation space
- Ease of cleaning and maintenance
Selecting the correct configuration helps achieve better screening accuracy and longer equipment life.
Common Applications in Manufacturing
A Vibro Shifter supports numerous production processes where material quality directly affects the finished product.
Typical applications include:
- Flour screening
- Spice powder separation
- Metal powder grading
- Resin screening
- Ceramic raw material processing
- Pigment classification
- Chemical powder separation
- Fertilizer screening
The versatility of the equipment makes it suitable for both small production facilities and large industrial plants.
Why Proper Screening Matters
Poor screening can lead to inconsistent product quality, equipment wear, production delays, and customer complaints. Oversized particles entering downstream machinery may also damage processing equipment or reduce manufacturing efficiency.
Using an appropriately designed Vibro Shifter helps eliminate these risks while improving process control and production reliability.
Many manufacturers in Navi Mumbai prefer working with experienced industrial equipment providers that understand the screening requirements of different industries. Companies such as Separation Engineers develop screening solutions that can be customized according to material characteristics, production capacity, and industry-specific standards, helping manufacturers achieve dependable and consistent results.